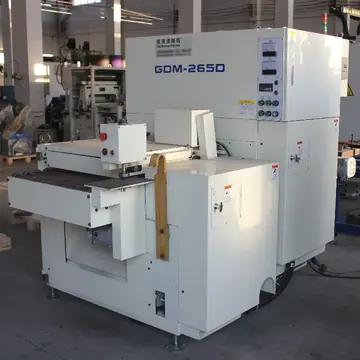
GDM-265DDeburring
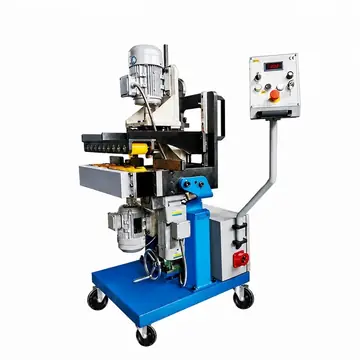
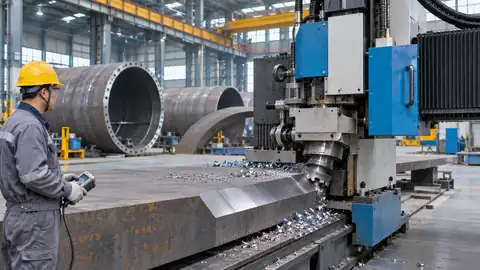
GDM-265D Automatic Plate Deslagging & Deburring Machine, 650 mm
- Plate thickness
- 9–100 mm
- Power
- 3,750 W
- Drive
- Electric
A GDM-265D removes dross from both faces of plasma-cut parts and a GCM-R3AR rounds the edges to R2 so the coating holds.
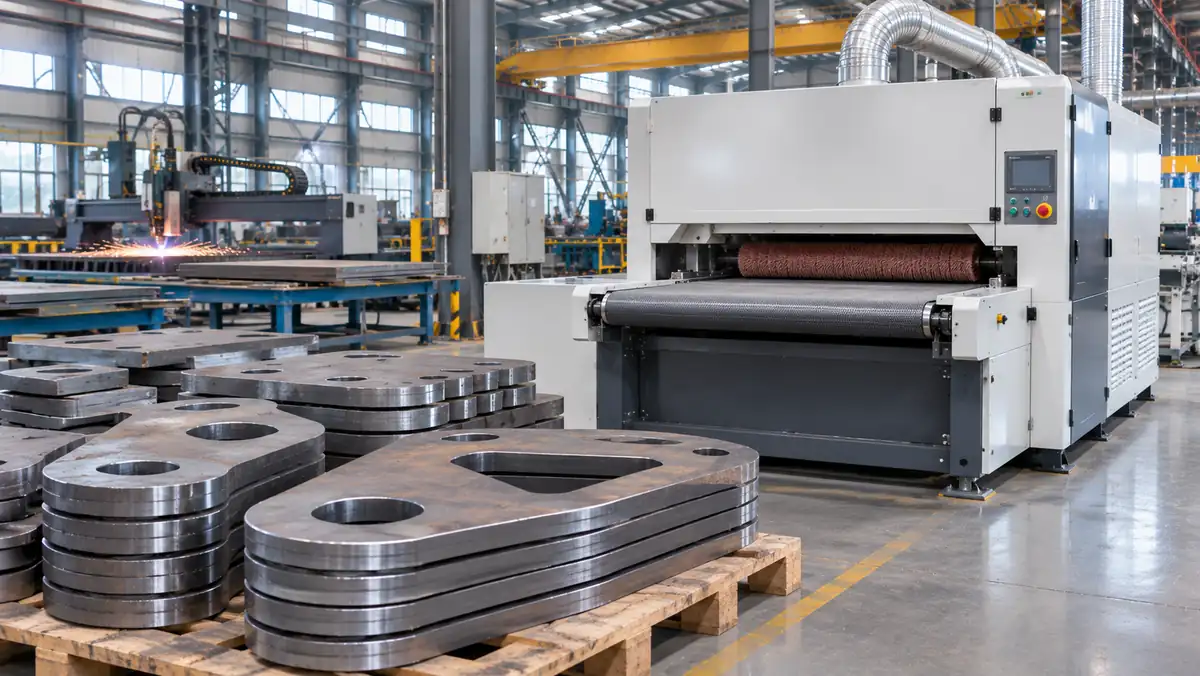
Coating systems for bridges and corrosive environments require rounded edges, and paint applied over cut-edge dross or sharp arrises thins out and fails first. Hand grinding hundreds of parts per shift is slow, inconsistent and hard on operators.
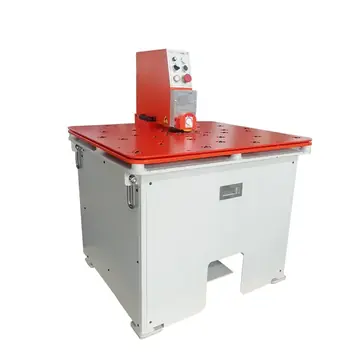
Parts leave the plasma table and pass through a GDM-265D, which strips dross and burrs from both faces, including around holes. Long edges are then rounded to R2 or R3 on a GCM-R3AR in one pass for both corners; small parts go over a table-type TCM-SR3-SP.
Consistent edge radius on every part and clean surfaces into the blast room, replacing manual grinding at this stage.
The equipment behind this application.
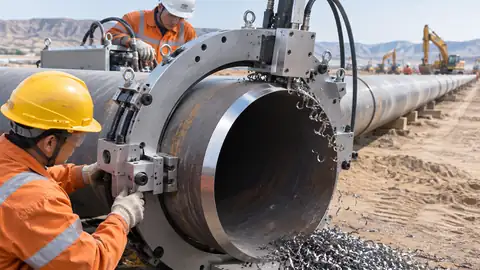
Split-frame OCE-630 machines cut out damaged sections and prepare weld-ready bevels on live-plant pipelines where hot work permits are restricted.
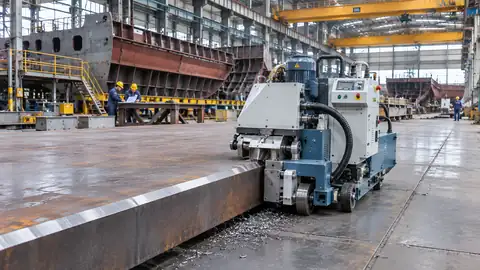
GMM-80R walking machines and a TMM-3000 CNC edge miller prepare K and X joints on hull plates without turning the plate over.
GMMA-100L and GMMA-100U machines mill deep U and J grooves on 60–100 mm shell plate, cutting filler metal compared with a V-groove.
Send us the scope and we will propose the machines, tooling and a quotation.