TMM-3000CNC Edge Milling
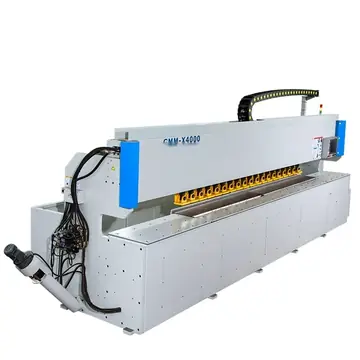
TMM-3000 CNC Double-Head Edge Milling Machine, 3 m Travel
- Plate thickness
- 6–80 mm
- Drive
- Electric
- Weight
- 6,500 kg
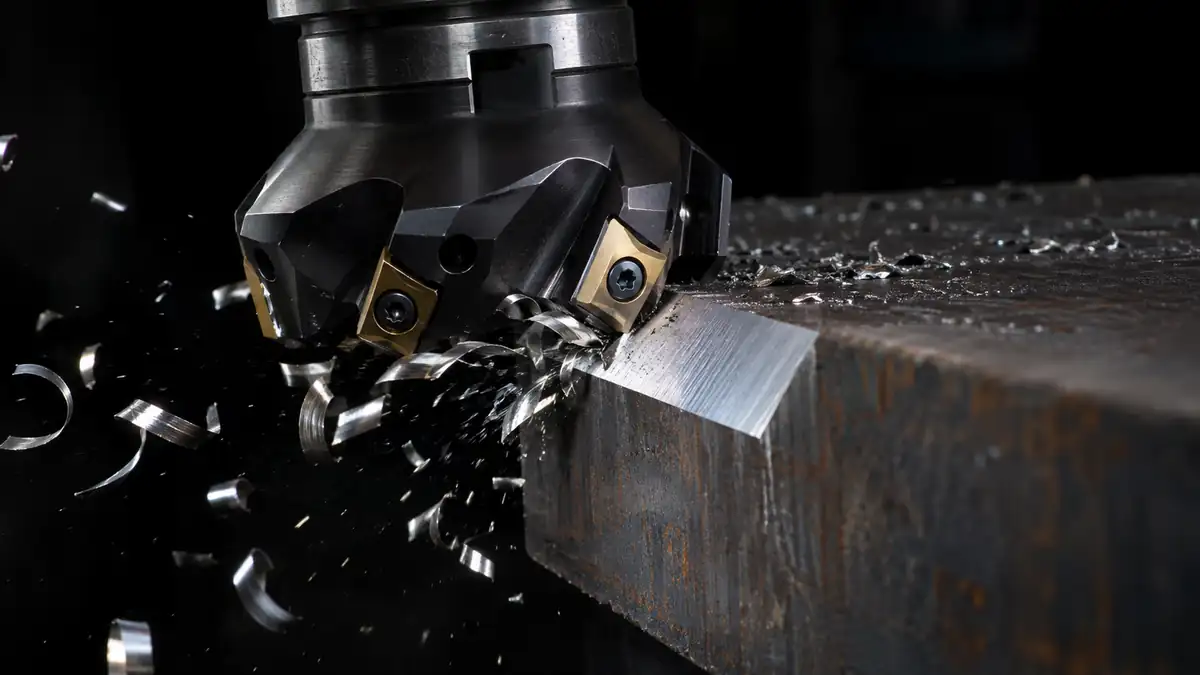
A TMM-3000 CNC edge miller bevels shell plates and a TFP-3000 machines large tower flanges flat after welding.
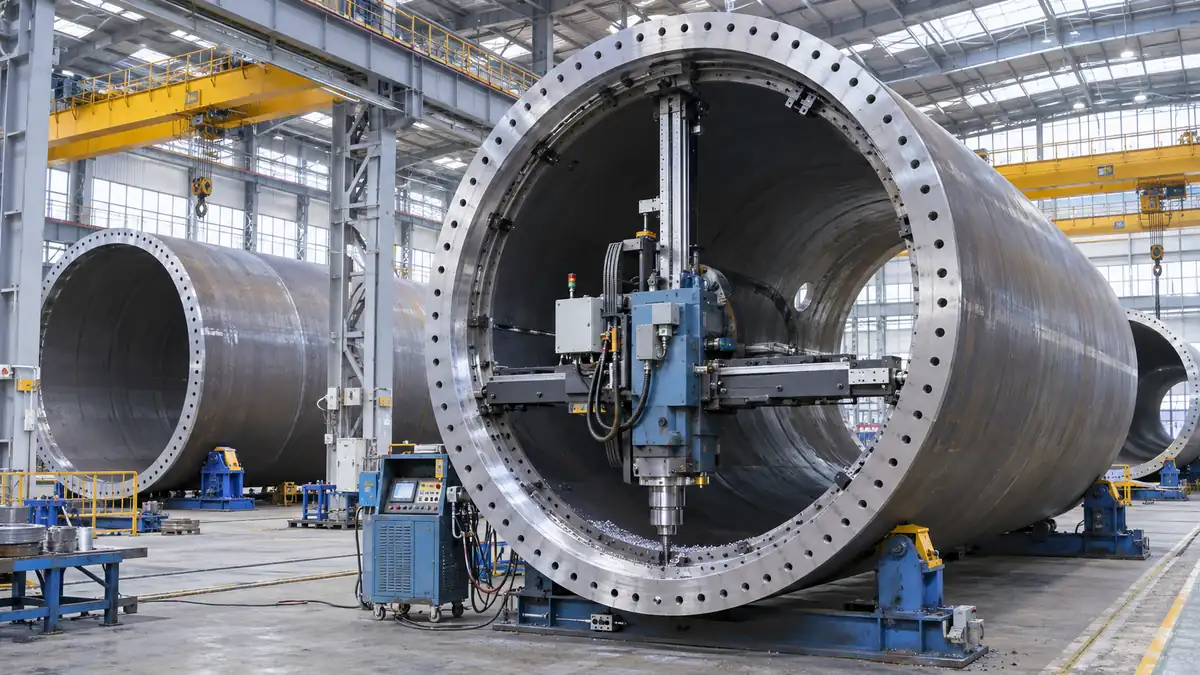
Tower shells are welded with submerged-arc welding, which needs uniform X or K preps along every longitudinal seam. After the flange is welded to the end can, welding distortion can take the flange out of flatness tolerance.
Shell plates are beveled on a TMM-3000 with both heads cutting the upper and lower bevels in one cycle. After welding, a TFP-3000 is mounted inside the tower flange to skim the face back to flatness, without moving the section to a vertical lathe.
Uniform bevels for automatic welding, and tower flanges brought back to flatness in place.
The equipment behind this application.
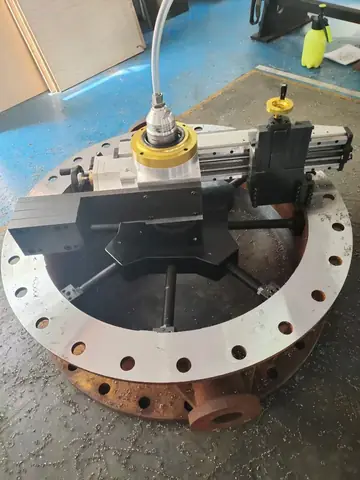
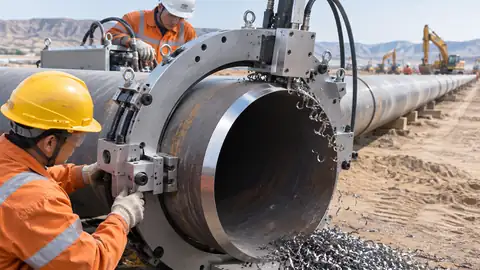
Split-frame OCE-630 machines cut out damaged sections and prepare weld-ready bevels on live-plant pipelines where hot work permits are restricted.
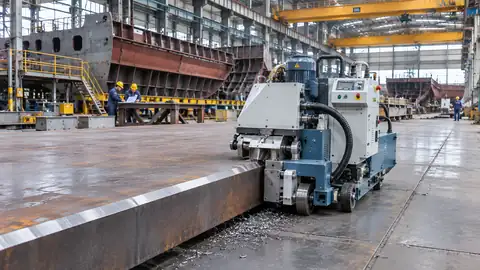
GMM-80R walking machines and a TMM-3000 CNC edge miller prepare K and X joints on hull plates without turning the plate over.
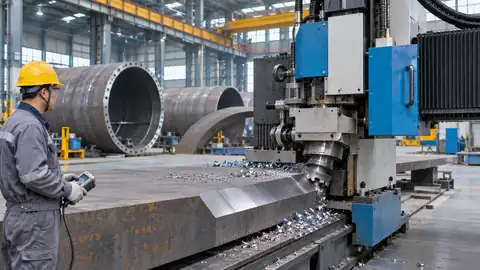
GMMA-100L and GMMA-100U machines mill deep U and J grooves on 60–100 mm shell plate, cutting filler metal compared with a V-groove.
Send us the scope and we will propose the machines, tooling and a quotation.